Understanding the new MoRTH guidelines
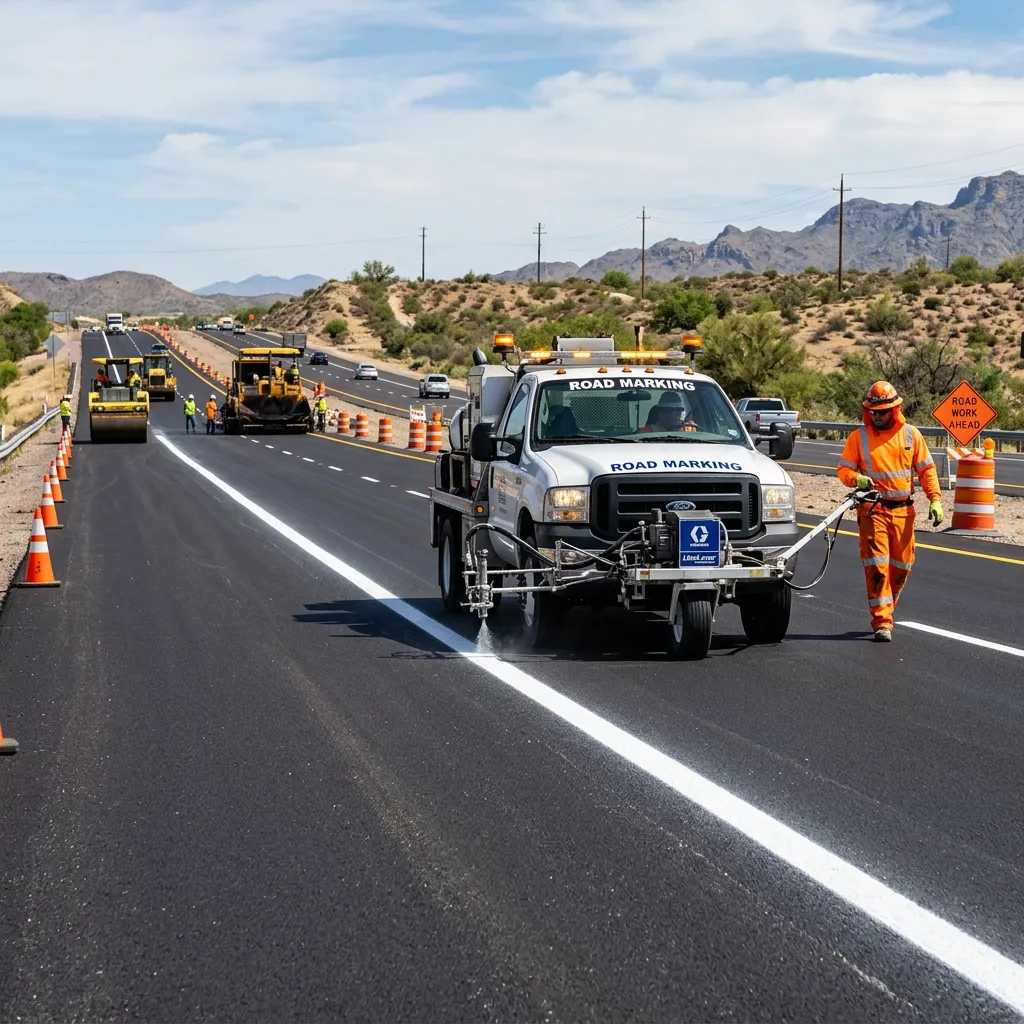
The Ministry of Road Transport and Highways (MoRTH) continuously updates its technical specifications to improve the durability and safety of Indian infrastructure. Staying ahead of these regulatory changes is non-negotiable for a Class-I contractor. Ignorance of the new MoRTH guidelines can lead to massive rejected works and financial ruin.
1 · Incorporating Reclaimed Asphalt Pavement (RAP) Sustainably
Implementing robust standards for incorporating reclaimed asphalt pavement (rap) sustainably requires aligning our field crews with standardized geotechnical and engineering procedures.
Incorporating Reclaimed Asphalt Pavement (RAP) into hot mix asphalt is a key focus under modern MoRTH guidelines for sustainable road construction. During pavement rehabilitation, specialized milling machines strip the old asphalt layer. This milled material is transported to our plant, screened, and blended with virgin aggregates and fresh bitumen binder. RAP contains aged binder that has oxidized over time, making it harder and more brittle. To offset this, we mix in rejuvenating agents to restore binder viscosity and elasticity. Utilizing RAP reduces the need for new aggregate quarrying and bitumen refining, lowering material costs and the carbon footprint of highway projects while meeting all structural and durability specifications for dense bituminous courses. We perform dynamic shear rheometer (DSR) testing on blended binders to verify performance, ensuring the recycled mix resists rutting and thermal cracking. This sustainable approach is aligned with PWD initiatives to promote eco-friendly contracting practices across Tamil Nadu.
Dense Bituminous Macadam (DBM) is a critical structural binder course laid between the road base and the wearing course. MoRTH specifications dictate aggregate gradation, binder content, and volumetric properties for DBM. The aggregate blend must consist of crushed stone and sand, combined to meet a specific grading envelope. The bitumen binder content typically ranges from 4.0% to 4.5% by weight of the mix. We run Marshall mix designs in our central lab to determine the optimum binder content that achieves the specified stability (minimum 9 kN) and flow value. In-place density is verified by core cutting, ensuring that field compaction matches at least 98% of the laboratory Marshall density to prevent rutting under heavy wheel loads. We also test for moisture susceptibility using tensile strength ratios (TSR), ensuring the mix resists water damage under heavy traffic loads. This technical compliance ensures the long-term durability of the pavement, preventing structural failure of the highway under heavy axle loads.
"Incorporating Reclaimed Asphalt Pavement (RAP) into hot mix asphalt is a key focus under modern MoRTH guidelines for sustainable road construction."
2 · Marshall Mix Design Optimization & Dense Macadam Specifications
Under our Coimbatore PWD quality guidelines, executing marshall mix design optimization & dense macadam specifications demands rigorous verification of all field metrics and material properties.
Laying Bituminous Concrete (BC) and Dense Bituminous Macadam (DBM) is a rigorous exercise in thermal control and mechanical execution. Hot mix asphalt is produced at temperatures between 150°C and 165°C using VG-30 or VG-40 bitumen binders. The workability of the mix is highly dependent on maintaining these elevated temperatures; as the mix cools, its viscosity increases exponentially. The rate of cooling during transport from the hot mix plant to the site is governed by ambient temperature, wind speed, dump truck bed insulation, and transit time. If the mix temperature drops below the critical threshold of 130°C before compaction begins, it becomes impossible to achieve the required density. This results in air-void ratios exceeding the maximum MoRTH limit of 4% to 6%, leading to high permeability, moisture stripping, and premature raveling. To mitigate this thermal loss, we mandate the use of heavy-duty insulated truck beds covered with triple-layer tarpaulins. We schedule laying operations during off-peak night shifts to avoid Coimbatore traffic delays, and use calibrated infrared thermal cameras to verify temperatures at the paver hopper. Rolling must occur in a tight, choreographed sequence: breakdown rolling at 140°C, intermediate compaction at 120°C, and finish rolling before the mix cools below 90°C.
Effective surface drainage is the single most critical factor in extending the service life of bituminous and concrete roads. Standing water penetrates asphalt, stripping the bitumen binder and creating potholes under traffic loads. We grade roadways with a precise cross-slope camber (typically 2-2.5% for asphalt roads and 1.5-2% for concrete roads) from the center crown to the shoulders. This cross-slope sheds water to concrete side drains. The longitudinal gradient must be kept above 0.3% to prevent water from pooling in side drains. Grade and slope checks are verified using electronic sensors on motor graders and checked manually using line-levels to ensure compliance with NHAI and MoRTH drainage standards. We also design and construct concrete culverts and catch basins at low points to channel runoff away from the roadway. The side drains are lined with stone masonry or precast concrete U-drains to prevent erosion of the shoulder, protecting the structural integrity of the pavement structure from water damage.
3 · Strict Laying Temperature Controls & Wind Cooling Prevention
To achieve maximum structural stability during the strict laying temperature controls & wind cooling prevention phase, we enforce strict compliance controls across our regional sites.
PWD projects are subject to strict quality control audits by departmental engineers and third-party testing agencies. Quality audits involve inspecting raw material test certificates, reviewing batch plant logs, and conducting in-situ tests. We maintain a mobile testing laboratory equipped to perform grain-size distribution, liquid limit, plastic limit, and compaction testing directly on-site. All test results are logged in a quality register signed by our QC engineer and the department representative. Maintaining this detailed quality record is a prerequisite for billing approvals, demonstrating our commitment to delivering infrastructure that meets PWD specifications. We also coordinate third-party inspections with independent testing labs, validating our field and laboratory test results. This quality assurance framework ensures that all construction works meet contractual quality standards, facilitating timely payment approvals and project sign-offs.
Maintaining comprehensive quality records is a core requirement for PWD and NHAI project compliance. Our project offices maintain registers for material receipts, concrete pours, compression test results, and level checks. Material delivery tickets, mill certificates, and third-party laboratory reports are filed systematically. These records are reviewed during inspections by departmental engineers, verifying that all materials and construction processes meet project specifications before billing approvals are granted. We also compile as-built surveys, quality logs, and contract documentation, preparing detailed project handbooks for municipal and state agencies. This rigorous drafting procedure supports our Class-I standing, ensuring quality compliance across all public works.
| Quality Verification Step | Audit Standard | Tolerance Benchmark / Compliance Target |
|---|---|---|
| Material Receipt Inspections | IS 383 Sieve Analysis | Zero organic contaminations; moisture grading within curves |
| Field Density Compactions | IS 2720 Part 28 Sand replacement | Minimum 98% field dry density versus lab standards |
| Concrete Cube Compressive Checks | IS 516 Compressive strength | Target 28-day crushing load exceeded on all cast cubes |
4 · Electronic Grader Sensor Controls & Drainage cams Grading
A major element of managing electronic grader sensor controls & drainage cams grading successfully lies in coordinating logistics, material testing, and machinery runtime.
Meticulous topographic surveying is the first step in successful site development and grading. Our engineering teams deploy Leica Total Stations and RTK (Real-Time Kinematic) GPS receivers to map site contours with millimeter accuracy. A high-density grid of elevation points is established, referencing permanent benchmarks linked to the national height datum. This digital spatial data is imported into CAD software to generate 3D digital terrain models (DTM) and calculate earthworks balances. Balancing cut-and-fill volumes minimizes the need to import expensive fill gravel or pay for hauling surplus soil off-site. Accurate stakeouts ensure that structural foundations, drainage channels, and roadway subgrades are excavated to the precise design coordinates and slopes, eliminating manual alignment errors and ensuring smooth surface drainage. During construction, we perform regular check-surveys to verify excavation depths and structural alignments, preventing deviations before concrete is poured. This digital workflow streamlines the client approval process and provides a precise as-built record for future site maintenance and expansion.
National Highways Authority of India (NHAI) packages demand meticulous quality documentation and progress-billing procedures. Payments are tied to strict physical milestones, such as completion of subgrade, Granular Sub-Base (GSB), Wet Mix Macadam (WMM), or bituminous paving layers. Generating monthly billing cycles requires cross-referencing survey data from RTK GPS Total Stations with daily material batching plant records. Quality control documentation, including compaction tests, bitumen extraction tests, and core-drilling logs, must accompany every invoice. Minor discrepancies in structural dimensions, level tolerances, or laboratory certifications can delay multi-crore disbursements for months. At Sri Vari, we maintain dedicated billing and QC coordination teams who document work in real-time, conduct joint measurements with independent engineers, and resolve level discrepancies proactively to maintain cash flow velocity. This digital record-keeping also provides a clear audit trail for third-party inspection agencies, ensuring compliance with all NHAI quality guidelines and contractual milestones. We also track machinery logbooks and fuel consumption to cross-verify productivity metrics against billed quantities, optimizing resource allocation across our highway packages.
5 · Operational Competency Auditing for PWD/NHAI Contracts
Ultimately, our site supervisors inspect every phase of operational competency auditing for pwd/nhai contracts to prevent structural settling and secure client sign-off.
Heavy construction machinery uptime is critical to meeting tight project timelines. Our fleet, including excavators, motor graders, soil compactors, and transit mixers, undergoes rigorous preventive maintenance. Soil and dust from excavation sites accelerate wear on track chains, pins, and rollers; we enforce daily undercarriage washdowns. Hydraulic systems are checked for pressure drops and water ingress, which can damage hydraulic pumps. Engine oil, filters, and air intake systems are serviced at designated running hour intervals (typically every 250 hours). By maintaining comprehensive service logs and stocking critical spares at our Coimbatore yard, we minimize on-site breakdowns and maintain high operational efficiency. We also train our operators to perform daily pre-start checks, monitoring coolant levels, hydraulic hoses, and warning indicators. This proactive maintenance culture ensures machinery availability and enhances site safety by preventing equipment failures during critical operations.
Successful infrastructure project execution depends heavily on supplier relations and material procurement logistics. Materials like cement, reinforcing steel (TMT bars), and aggregate represent over 60% of project costs. We leverage our Class-I standing to secure bulk pricing and direct mill shipments from primary steel and cement manufacturers. To maintain continuous supply, we establish long-term contracts with regional blue metal crushers and M-sand plants. Structured payment terms, backed by corporate bank guarantees, ensure priority supply during seasonal material shortages. Material haulage is optimized using GPS-tracked dumpers to coordinate dispatch from crushers to the paving site, ensuring that asphalt pavers and concrete batching plants operate continuously without logistical delays. We also maintain on-site material stockpiles to buffer against supply disruptions, and inspect incoming material quality to ensure compliance with project specifications. This coordinated logistical approach minimizes project delays and protects our margins from material price volatility.
6 · Strict Volumetric Testing & Quality Assurance Documentation
Furthermore, daily reporting and quality logging are mandated to maintain complete project visibility and contract compliance.
Managing dump truck dispatch logistics is essential for large-scale earthwork and paving projects. We operate a fleet of 10-ton and 20-ton tippers, coordinated using a central logistics platform. GPS tracking provides real-time visibility into truck positions, travel speeds, and cycle times. We analyze this data to identify bottlenecks at loading quarries or site dumping zones. By adjusting dispatch intervals and rerouting trucks around traffic, we maintain a steady flow of materials to the paving site, maximizing machinery utilization and minimizing project timelines. We also monitor fuel efficiency and driver shift compliance, using fleet diagnostics to manage operating costs. This logistical control ensures aggregate deliveries align with paving rates, maximizing highway paving efficiency.
Incorporating Reclaimed Asphalt Pavement (RAP) into hot mix asphalt is a key focus under modern MoRTH guidelines for sustainable road construction. During pavement rehabilitation, specialized milling machines strip the old asphalt layer. This milled material is transported to our plant, screened, and blended with virgin aggregates and fresh bitumen binder. RAP contains aged binder that has oxidized over time, making it harder and more brittle. To offset this, we mix in rejuvenating agents to restore binder viscosity and elasticity. Utilizing RAP reduces the need for new aggregate quarrying and bitumen refining, lowering material costs and the carbon footprint of highway projects while meeting all structural and durability specifications for dense bituminous courses. We perform dynamic shear rheometer (DSR) testing on blended binders to verify performance, ensuring the recycled mix resists rutting and thermal cracking. This sustainable approach is aligned with PWD initiatives to promote eco-friendly contracting practices across Tamil Nadu.
Operational Summary & Takeaways
This concludes our comprehensive analysis on understanding the new morth guidelines. At Sri Vari Constructions, we understand that delivering high-performance infrastructure requires a combination of advanced engineering, rigorous quality assurance, and deep local geological knowledge. As a licensed Class-I Civil Contractor serving Coimbatore, Tiruppur, Erode, and the wider Kongu region, we adhere strictly to the latest Ministry of Road Transport and Highways (MoRTH) standards, Tamil Nadu Public Works Department (PWD) specifications, and NHAI quality guidelines. By maintaining a privately owned fleet of over 85 machinery units—including hydraulic excavators, motor graders, and vibratory compactors—and employing experienced site engineers, we ensure that every project we undertake is built to last. Our commitment to daily reporting, strict safety protocols, and robust engineering standards has established us as a trusted partner for public works and private industrial site developments across Tamil Nadu.